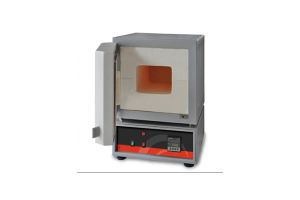
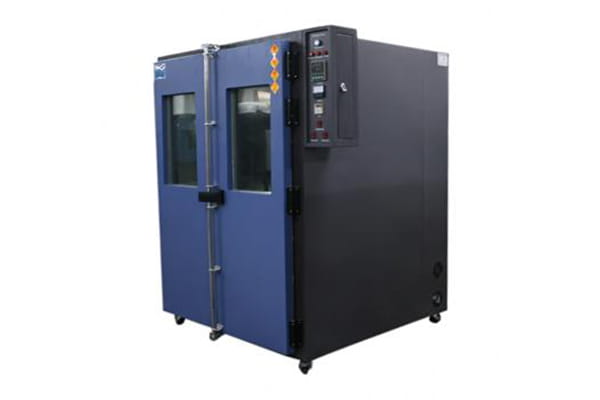
An Industrial Oven is an insulated, temperature-controlled process chamber used for drying, curing, baking, preheating, ageing and other controlled thermal operations. Marjan Polymer Industries (MPI) designs and supplies custom batch, cabinet, walk-in and conveyor ovens for manufacturers and laboratories in Pakistan.
The oven is engineered from the product load, required part-temperature profile, chamber size, airflow, exhaust, heat source, production rate and safety classification. A controller setpoint alone does not establish process uniformity; airflow and loaded temperature mapping are central to the design.
Thermal Process Purpose
Forced convection transfers heat from the recirculated air to the workpiece. The system must bring the full load to the required temperature, hold it for the defined time and remove moisture or process vapours at a controlled rate. Heating capacity, air velocity, loading pattern, exhaust and recovery time are therefore selected as one thermal system.
Industrial Oven Configurations
| Configuration | Typical use | Available options |
|---|---|---|
| Cabinet/batch oven | Trays, racks, components and flexible batch work | Single/double door, shelves, trolley, data logger and programmable recipe |
| Walk-in oven | Large assemblies, wheeled racks and high-mass loads | Floor tracks, reinforced floor, ramp, pass-through doors and multiple circulation zones |
| Conveyor oven | Continuous curing, drying or preheating | Belt/chain/overhead conveyor, staged zones, cooling and line interlocks |
| Tray dryer/hot-air oven | Powders, granules and components on controlled trays | Filtered make-up air, adjustable exhaust and hygienic contact surfaces where required |
| Special-atmosphere oven | Selected inert, low-oxygen or vacuum-assisted processes | Requires separate pressure, gas, purge, leak and hazard engineering |
Configurable Technical Range
| Parameter | Common project range | Selection basis |
|---|---|---|
| Operating temperature | Approximately ambient +20 °C to 300 °C for common forced-convection ovens; systems to approximately 500–600 °C by special review | Product, insulation, fan, seals, sensors, heater and construction materials |
| Chamber volume | Approximately 0.1–50 m³; smaller or larger custom chambers available | Load envelope, rack/trolley, air passages and production batch |
| Temperature uniformity | Typically ±3 to ±10 °C at agreed setpoints and qualified conditions | Chamber, load, sensor grid, airflow, soak time and test standard |
| Control accuracy | Typically ±0.5 to ±2 °C at the control sensor | Controller, sensor, electrical design and calibration |
| Heating | Electric, indirect gas or direct gas where the process permits | Temperature, energy source, product contamination, ventilation and safety code |
| Air exchange | Adjustable make-up and exhaust; forced exhaust where required | Moisture/volatile release, chamber pressure and safe concentration |
Airflow and Heat-Transfer Design
- Horizontal, vertical or combination airflow selected from load geometry and rack arrangement.
- Recirculation fan and supply/return plenums sized for temperature distribution and pressure drop.
- Adjustable baffles or nozzles for field balancing where required.
- Fresh-air and exhaust control for moisture removal, vapour dilution and chamber pressure.
- Optional staged heating, controlled cooling and product-temperature thermocouples.
Construction and Insulation
| Element | Project options |
|---|---|
| Interior | Galvanised steel, aluminised steel or stainless steel selected from temperature, corrosion and cleanliness |
| Exterior | Coated mild steel or stainless steel panels on a structural frame |
| Insulation | Mineral wool, ceramic fibre or layered system with thickness selected from operating temperature and surface-temperature target |
| Doors | Hinged, double, vertical-lift or pass-through with high-temperature seals and safety release where required |
| Loading | Shelves, trays, trolley, rack, reinforced floor, rail or conveyor interface |
Controls and Data
- PID temperature control with high-limit over-temperature protection independent of the process controller.
- Programmable ramps, dwells and recipes for repeatable curing or ageing cycles.
- Door, fan, heater/burner, exhaust and conveyor interlocks.
- Multi-point recording, batch report, alarms and optional remote/plant data interface.
- Product thermocouples, humidity or pressure monitoring when required by the process.
Applications in Pakistan
- Paint, powder-coating, adhesive, resin and composite curing.
- Rubber post-curing, plastic drying/preheating and component ageing.
- Electrical/electronic component baking and moisture removal.
- Metal-part preheating, stress-relief or heat-treatment duties within the approved oven range.
- Textile, chemical, pharmaceutical or food processes only with suitable hygienic, exhaust and validation design.
- Laboratory scale-up, production development and quality-control thermal cycles.
Safety Classification
Any process that releases flammable solvent, combustible vapour, dust or gas requires a dedicated hazard review. The scope may require powered exhaust, purge timing, airflow proving, dilution calculations, explosion relief, burner-management functions and safe electrical equipment. A standard non-volatile oven must not be used for such a process.
Safeguards can include over-temperature cut-out, fan/airflow proving, door interlock, emergency stop, heater contactor monitoring, burner flame supervision, pressure relief and safe-access release, selected from the final risk assessment and applicable requirements.
Factory Acceptance and Temperature Mapping
| Test | Typical scope |
|---|---|
| Construction inspection | Dimensions, door, insulation, fan, heater, guards and control-panel checks |
| Functional FAT | Warm-up, controls, alarms, interlocks, fan/exhaust and programmed cycle |
| Empty-chamber mapping | Multi-point survey at agreed setpoints after stabilisation |
| Loaded mapping | Performed only with an agreed representative load, rack pattern and method |
| Documentation | Drawings, operating manual, electrical diagram, calibration and recommended spare parts |
Information Required for a Proposal
- Product/material, load dimensions and mass, rack/tray/trolley arrangement and batch size.
- Starting, set and maximum temperature; heat-up, soak, cooling and total-cycle targets.
- Moisture, solvent or volatile release with safety data and maximum release rate.
- Required uniformity, mapping standard, sensor locations and reporting/validation needs.
- Available electric/gas utilities, ventilation, floor space and installation location in Pakistan.
Installation and After-Sales Support
MPI can provide site-interface review, installation supervision, commissioning, temperature mapping support, operator training and preventive-maintenance guidance in Pakistan. Civil work, duct route, gas train, electrical feeder and customer responsibilities are identified in the approved project documents.
Frequently Asked Questions
What is an Industrial Oven?
An Industrial Oven is an insulated process chamber that applies controlled heat for drying, curing, baking, preheating, ageing or related production and laboratory operations.
What is the difference between an oven and a furnace?
Ovens commonly use forced convection at low to medium temperatures, while high-temperature furnaces rely more heavily on radiant heat and refractory construction. The process temperature and material determine the correct equipment.
What temperature range can MPI provide?
Many forced-convection projects operate from approximately ambient +20 °C to 300 °C. Special ovens may reach about 500–600 °C, but fans, insulation, seals, sensors and construction must be selected for the rated temperature.
How is temperature uniformity specified?
Uniformity must state the setpoint, load or empty condition, sensor positions, stabilisation time and mapping method. A typical project class may be ±3 to ±10 °C, subject to chamber and process design.
Can the oven be electric or gas heated?
Yes. Electric, indirect gas and selected direct-gas systems can be evaluated. Energy availability, temperature, product contamination and safety classification guide the choice.
Can MPI manufacture a walk-in or conveyor oven?
Yes. Cabinet, batch, walk-in, trolley and conveyor configurations can be engineered around the load, production rate, plant layout and material-handling method.
Can an oven handle solvent-based products?
Only a specially engineered oven may handle flammable volatiles. Exhaust, purge, airflow proving, vapour release, explosion relief and applicable safety requirements must be reviewed before design.
Is temperature data logging available?
Yes. Programmable recipes, multiple thermocouples, alarms, batch reports and plant data interfaces can be included in the control specification.
Does MPI provide installation in Pakistan?
MPI can provide installation supervision, commissioning, mapping support, training and after-sales service in Pakistan according to the project scope.
What information is needed for a quotation?
Provide the load, chamber/rack dimensions, temperature profile, cycle time, uniformity requirement, volatile release, heating preference, utilities and installation location.
Request an Industrial Oven Proposal
Send MPI your load dimensions and mass, process temperature profile, uniformity requirement, production cycle, volatile information, heating preference and site conditions. Marjan Polymer Industries will prepare a project-specific Industrial Oven proposal for your facility in Pakistan.