Cold Galvanizing vs Traditional Paint and Hot-Dip Galvanizing
Cold galvanizing compound, conventional paint and hot-dip galvanizing are three different corrosion-control approaches. The correct choice depends on the steel condition, whether fabrication can enter a galvanizing plant, the exposure environment, required appearance, repair area, inspection plan and expected maintenance strategy.
Reviewed: 29 August 2026
Evidence basis: Current manufacturer data, ASTM A780/A780M and ISO 1461.
Quick answer: Hot-dip galvanizing forms a metallurgically bonded zinc coating in a controlled plant process. A cold galvanizing compound is a zinc-rich coating applied to correctly prepared steel in the shop or field. Conventional paint primarily protects by maintaining a continuous barrier film. None of these descriptions makes one method a universal replacement for the others.
Three Different Protection Mechanisms
Hot-dip galvanizing immerses fabricated steel in molten zinc. The process forms zinc-iron alloy layers and an outer zinc layer that provide barrier and sacrificial protection. Component design, venting, drainage, bath access, transport and distortion risk must be considered before galvanizing.
Cold galvanizing compound is applied by brush, roller or suitable spray equipment at ambient temperature. Its galvanic contribution depends on a high metallic-zinc content, electrical continuity within the cured film and direct contact with clean steel. Oil, salts, rust, mill scale, dust or an intervening non-conductive coating can prevent the intended performance.
Conventional paint systems normally use one or more compatible coats to isolate steel from moisture, oxygen and contaminants. Properly engineered primers, intermediate coats and topcoats can provide colour, chemical resistance, UV stability or immersion resistance. Their protection mechanism and repair requirements depend on the complete specified system.
Technical Comparison
| Decision factor | Cold galvanizing compound | Conventional paint system | Hot-dip galvanizing |
|---|---|---|---|
| Application location | Shop or field | Shop or field | Specialist galvanizing plant |
| Primary protection | Metallic-zinc galvanic action plus barrier | Primarily barrier protection; chemistry depends on the system | Metallurgically bonded zinc coating with barrier and sacrificial action |
| Steel condition | Clean exposed metal with suitable surface profile | Preparation defined by the selected coating specification | Fabricated steel designed and prepared for the galvanizing process |
| Typical practical role | Galvanizing repair, welds, cut edges, installed steel and maintenance | Colour, specialised resistance and engineered multi-coat protection | New fabricated components that can be processed in a plant |
| Appearance | Normally grey or product-specific metallic finish | Wide colour and gloss range | Metallic zinc appearance that changes as it weathers |
| Critical control | Metal contact, mixing, dry-film thickness and cure | Preparation, compatibility, coverage and recoat windows | Fabrication design, process control, coating continuity and repair |
When Each Method Is Appropriate
Choose hot-dip galvanizing when
- Newly fabricated components can be transported to and processed by a galvanizing plant.
- The design provides correct venting, drainage and access for the galvanizing process.
- The project requires a factory-applied zinc coating under a defined galvanizing specification.
Choose a cold galvanizing compound when
- Damaged galvanized coating, welds, cut edges or local bare-steel areas require repair.
- Installed steel cannot practically be immersed in a galvanizing bath.
- The governing specification permits a zinc-rich paint repair method.
- Surface preparation, film thickness and inspection can be controlled in the field or workshop.
Choose an engineered paint system when
- Colour, gloss retention, chemical resistance or immersion exposure drives the selection.
- A compatible primer, intermediate coat and topcoat system has been specified.
- Inspection and future maintenance will follow the coating manufacturer’s requirements.
Surface Preparation and Quality Control
Surface preparation is not interchangeable between these methods. A cold galvanizing compound intended to provide galvanic protection normally needs direct contact with prepared steel. Existing paint, grease, soluble salts, corrosion products, mill scale, moisture and dust must be removed to the level required by the current product data and project specification.
Quality control should record the preparation method, ambient conditions, substrate temperature, mixing, thinning where permitted, wet- or dry-film thickness, recoat interval and final inspection. A high zinc percentage cannot compensate for contamination, an unsuitable surface profile or inadequate film thickness.
Repairing Damaged Hot-Dip Galvanizing
ASTM A780/A780M identifies zinc-based solders, zinc-rich paints and sprayed zinc as repair-material categories for damaged or uncoated areas of hot-dip galvanized coatings. Project parties must still agree the permitted repair method, preparation, repair extent and acceptance criteria.
ISO 1461:2022 addresses batch hot-dip galvanized coatings and contains repair provisions. Applying zinc-rich paint does not convert the repaired area into a metallurgically bonded hot-dip coating. Performance language should therefore describe the approved repair system accurately rather than claim that cold-applied material is identical to factory galvanizing.
A Verified ROVAL R Example
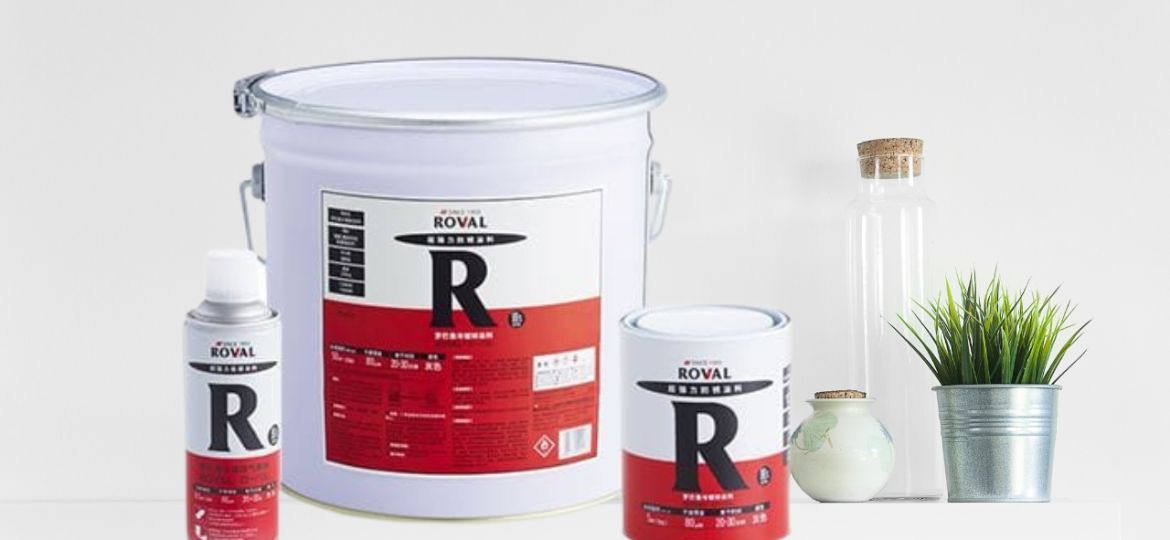
ROVAL R is a single-component cold galvanizing compound manufactured in Japan. The current manufacturer technical data states 96% ±1 zinc by weight in the dry film and a standard total dry-film thickness of approximately 80 µm in two coats of about 40 µm each. Product-specific preparation, environmental limits, drying, application and safety instructions must come from the current ROVAL documents.
Common Specification Errors
- Calling any grey metallic paint “cold galvanizing” without confirming metallic-zinc content and intended mechanism.
- Using the terms cold galvanizing and hot-dip galvanizing as if the coating structures were physically identical.
- Applying a galvanic zinc coating over intact non-conductive paint when direct metal contact is required.
- Quoting durability without an exposure category, surface-preparation standard, film thickness and maintenance assumptions.
- Selecting by purchase price alone while ignoring transport, shutdown, inspection and future repair costs.
Frequently Asked Questions
Is cold galvanizing equal to hot-dip galvanizing?
No. Both can use zinc for sacrificial protection, but their application process, coating structure, abrasion behaviour and quality-control requirements are different.
Can cold galvanizing compound be applied over paint?
Not where the system requires direct galvanic contact with steel. The application area normally has to be returned to suitably prepared exposed metal unless the manufacturer has approved a different system.
Which method is suitable for welded field repairs?
A specified zinc-rich repair coating is often practical for welds and local damaged areas when the governing standard permits it and preparation, thickness and inspection are controlled.
Can conventional paint be applied over a zinc-rich coating?
Only when the complete coating system is compatible and the manufacturer’s curing, preparation and recoat requirements are satisfied.
Which corrosion-protection method lasts longest?
There is no universal answer. Exposure, fabrication design, preparation, coating thickness, application quality, mechanical damage, inspection and maintenance all affect service life.
ROVAL R Product Data and Supply in Pakistan
For verified technical values, the current 2.5 kg product, price, stock and nationwide supply information, use the dedicated product page.
Technical References
- ROVAL R Technical Data Sheet
- ROVAL R Safety Data Sheet
- ASTM A780/A780M — repair of damaged galvanized coatings
- ISO 1461:2022 — hot-dip galvanized coatings
Technical notice: This guide does not replace the current manufacturer TDS, SDS, contractual coating specification or site-specific engineering assessment.
