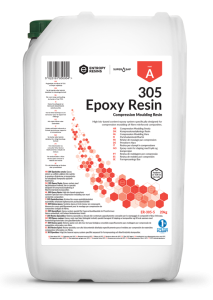
Prepreg epoxy resin is the engineered matrix that binds carbon, glass or aramid reinforcement in a controlled fibre–resin system. Marjan Polymer Industries supports composite manufacturers, research laboratories and product-development teams in Pakistan with application-matched prepreg materials and resin systems, technical selection and process guidance.
What Is Prepreg Epoxy Resin?
“Prepreg” means a reinforcing fibre that has already been impregnated with a measured amount of resin and is supplied in a controlled, partially advanced state for later forming and cure. Depending on the manufacturing route, the requirement may be a ready-to-use carbon, glass or aramid prepreg; a one-component hot-melt matrix resin for a prepregging line; or a qualified two-component impregnation system. These are different supply forms and must not be treated as interchangeable.
The correct grade is selected against reinforcement, manufacturing method, cure equipment, service environment and certification needs. Cure temperature, out-life, storage life, resin content, tack, flow and final glass-transition temperature are grade-specific values confirmed in the applicable technical data sheet.
Available Supply Routes
- Ready-made epoxy prepreg: carbon, glass or aramid reinforcement supplied with controlled resin content and process history.
- One-component prepreg matrix: formulated for controlled hot-melt or supported impregnation processes and B-stage handling.
- Two-component impregnation resin: selected for qualified in-house impregnation, filament winding or development work where the process permits mixing immediately before use.
- Application-matched sourcing: systems shortlisted by cure window, storage conditions, mechanical targets and production volume.
Reinforcement and Product Options
| Requirement | Available engineering direction |
|---|---|
| Reinforcement | Carbon fibre, E-glass, S-glass, aramid and selected technical fabrics |
| Architecture | Unidirectional tape, woven fabric, multiaxial fabric and application-specific preforms |
| Resin content | Specified by the selected grade, fibre areal weight and laminate design |
| Cure route | Autoclave, vacuum-bag oven, heated press or other qualified process |
| Performance priorities | Toughness, thermal performance, optical finish, flame/smoke behaviour or structural strength |
| Supply basis | Trial quantity, research supply or production-scale sourcing subject to grade and availability |
Critical Selection Parameters
A useful specification begins with the finished component, not a generic resin number. MPI reviews the following parameters before recommending or sourcing a system:
- target fibre type, weave, areal weight and laminate thickness;
- required tack, drape, resin flow and consolidation behaviour;
- cure temperature, dwell time, ramp rate and available pressure or vacuum;
- required glass-transition temperature, mechanical performance and environmental resistance;
- working life, shop-floor out-life, freezer shelf life and transport cold-chain capability;
- surface finish, void-content target and dimensional tolerance;
- applicable aerospace, automotive, defence, sports, electrical or research qualification requirements.
Processing Workflow
- Define the laminate: confirm reinforcement, ply sequence, fibre orientation and performance target.
- Select the resin/prepreg grade: match chemistry, cure window, tack, drape and storage needs to the process.
- Control storage: maintain the grade-specific frozen or refrigerated storage condition and a traceable inventory log.
- Condition before opening: allow sealed material to reach the specified handling temperature before opening to reduce condensation risk.
- Lay-up and debulk: follow approved ply placement, release, breather and vacuum-bag procedures.
- Cure and cool: use the supplier-approved temperature, pressure/vacuum, dwell and cooling cycle.
- Inspect: verify cure records, thickness, surface quality and any required non-destructive or mechanical test results.
Quality-Control Checks
Receiving and process controls can include certificate-of-analysis review, batch and expiry verification, resin content, volatile content, gel time, resin flow, tack and drape, differential scanning calorimetry, freezer-temperature records and laminate coupon testing. The exact plan should reflect the risk and qualification level of the component.
Typical Applications
- lightweight carbon-fibre structural panels and components;
- automotive, motorsport and transport composite parts;
- industrial tooling, fixtures and high-performance laminates;
- pressure, electrical and thermal composite structures where a qualified grade is available;
- sports equipment and precision moulded products;
- university, defence and industrial composite research in Pakistan.
Storage, Handling and Safety
Prepreg materials commonly require controlled cold storage, but the required temperature and shelf life differ by grade. Use the manufacturer’s current technical and safety data sheets, maintain batch traceability and wear the specified personal protective equipment. Avoid uncontrolled warming and refreezing. Thaw sealed packages before opening, return unused material within its permitted exposure time and record cumulative out-life.
Why Source Through Marjan Polymer Industries?
- Pakistan-based technical discussion and requirement capture;
- selection by application and process rather than unsupported headline values;
- support for resin, reinforcement, consumables and composite-processing equipment;
- trial-to-production sourcing pathways, subject to grade availability;
- documentation review for storage, cure and quality-control planning.
Information Required for a Quotation
Please share the reinforcement type and areal weight, component and application, required resin content or prepreg format, annual or trial quantity, preferred cure equipment and temperature, mechanical or thermal targets, storage capability, applicable standards and delivery location in Pakistan. MPI will then confirm the feasible material route, commercial basis and lead time.
Frequently Asked Questions
Is prepreg epoxy resin the same as liquid laminating epoxy?
No. A prepreg matrix is engineered for controlled fibre impregnation, storage and later cure. A general laminating resin may not provide the required B-stage, tack, flow, out-life or storage behaviour.
Can MPI supply carbon-fibre prepreg in Pakistan?
MPI can evaluate carbon, glass and aramid prepreg requirements and source an appropriate grade subject to reinforcement format, cure window, quantity, documentation and availability.
Is the material supplied as one component or two components?
Both routes exist. Commercial ready-to-use prepreg and many hot-melt matrix systems are supplied as controlled one-component materials, while some in-house impregnation processes use qualified two-component systems. The supply form is confirmed before quotation.
What cure temperature is required?
There is no universal cure temperature. It is defined by the selected resin or prepreg grade and must be followed from the approved technical data sheet and cure schedule.
Does prepreg always require an autoclave?
No. Some grades are designed for vacuum-bag oven, heated-press or out-of-autoclave processing. Equipment compatibility must be confirmed during grade selection.
How should prepreg be stored?
Many grades require frozen or refrigerated storage with logged temperature control. The exact temperature, shelf life and permitted out-life are grade-specific.
Can the resin content and fibre format be customized?
Where the manufacturing source permits, reinforcement type, areal weight, width, architecture and target resin content can be specified. Minimum quantity and technical feasibility apply.
Which information is needed to select a grade?
Provide reinforcement, laminate design, cure equipment, operating environment, mechanical and thermal targets, quantity, standards and storage capability.
Can MPI support laboratory development quantities?
Trial or research quantities may be possible depending on grade and source. MPI can also help define a scale-up specification for later production supply.
Which technical documents and tests should be reviewed before approval?
Review the current technical and safety data sheets, batch traceability, storage and out-life requirements, cure schedule and laminate test data. Structural approval should use coupons made from the selected reinforcement, resin content and production cure cycle.