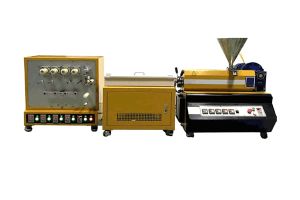

The Single Screw Extruder is a compact rubber-processing machine for continuously conveying prepared compound through a screw and barrel, building controlled pressure and forming the material through a selected die. The reference machine on this page is a 30 mm hot-feed configuration intended for laboratory work, formulation development, profile trials and controlled small-batch production.
Marjan Polymer Industries supplies single screw extruder machines in Pakistan for rubber laboratories, product-development departments, universities and manufacturing plants. The screw, barrel, die head, drive, cooling arrangement and controls are reviewed against the compound, required profile, production rate and upstream preparation method before the machine is finalized.
The 30 mm data shown below defines the reference configuration represented by the existing machine record. Alternative diameters, feed systems and production arrangements are separate engineered configurations and must not be assumed to deliver the same output or process every rubber compound.
Purpose and applications
- Laboratory extrusion and rubber-compound evaluation
- Development of seals, gaskets, strips, cords and continuous profiles
- Small-batch trials before committing material to a production line
- Die and profile-development work
- Evaluation of compound flow, surface quality and dimensional stability
- Educational and research use in polymer and rubber-processing laboratories
- Feeding compatible downstream forming or testing equipment when included in the approved process
Reference 30 mm configuration
| Design item | Reference machine data |
|---|---|
| Machine type | Compact hot-feed single screw rubber extruder |
| Screw arrangement | Single screw and barrel |
| Reference screw diameter | 30 mm |
| Reference screw-speed range | 0–80 rpm, adjustable |
| Indicative maximum output | Up to approximately 15 kg/h, dependent on compound, feed condition, die and operating settings |
| Reference drive motor | 2 kW |
| Gearbox | Heavy-duty oil-immersed reduction gearbox |
| Driving head | Independent drive-head arrangement |
| Barrel temperature management | Dual-jacketed water-cooling arrangement |
| Frame | Fabricated steel machine structure |
| Wetted or working-component material | Engineering steel or stainless-steel selection according to compound, wear and contamination requirements |
| Control approach | Variable screw-speed control with electrical protection; final instruments and interlocks confirmed in the quotation |
How the single screw extrusion process works
Prepared rubber compound enters the feed section and is gripped by the rotating screw. The screw conveys and works the material through the barrel while the machine controls the process temperature. Pressure develops toward the head, forcing the compound through a die that defines the initial cross-section of the extrudate.
The final profile depends on compound behaviour, screw geometry, die design, head pressure, screw speed and downstream handling. Rubber normally changes dimensions after leaving the die, so die swell, shrinkage and the subsequent cooling or vulcanization process must be considered during profile development.
Hot-feed and cold-feed selection
| Feed approach | Engineering consideration |
|---|---|
| Hot-feed reference machine | Receives rubber that has already been warmed and prepared, commonly by upstream mixing or milling equipment. The reference 30 mm configuration on this page is presented on this basis. |
| Cold-feed alternative | Uses a screw, feed system, drive and temperature-control design selected to accept compound closer to ambient temperature. It is a separate configuration, not merely a change of operating setting. |
| Vented or pin-barrel systems | Used for applications requiring additional mixing, degassing or process control. Suitability is reviewed against the compound and product. |
MPI confirms the feed method only after reviewing the rubber formulation, batch form, upstream equipment, required output and profile quality. A hot-feed machine should not be ordered for a cold-feed process without a full engineering review.
Configurable engineering options
| Selection item | Available engineering approach |
|---|---|
| Screw and barrel | Geometry, compression behaviour, surface treatment and material selected for the stated rubber compound and duty |
| Die and head | Profile die, tube or hose head, strip die, cord head, strainer head or customer-specific tooling after product review |
| Drive | Motor, gearbox, speed range and torque selected for screw diameter, compound and pressure requirement |
| Temperature management | Cooling jackets, circulating-water unit and additional controlled zones as required by the approved process |
| Instrumentation | Screw-speed indication, temperature indication, motor-load monitoring and melt/head-pressure protection where specified |
| Feeding | Manual prepared-strip feed or engineered feed assistance according to machine size and compound form |
| Controls | Conventional control panel or PLC/HMI package with project-specific alarms and interlocks |
| Downstream scope | Cooling, haul-off, cutting, collection or vulcanization equipment quoted separately when required |
Rubber compounds and profile applications
Single screw rubber extruders may be configured for natural-rubber and synthetic-rubber compounds used in seals, gaskets, strips, hoses, tubes, cords, cable coverings, automotive profiles and other continuous products. Actual compatibility depends on formulation, filler loading, viscosity, scorch behaviour, feed preparation and the required surface finish.
Silicone, highly abrasive compounds, sponge profiles, compounds containing sensitive additives and materials requiring degassing can need different screw, barrel, venting, temperature control or downstream curing arrangements. MPI reviews the compound information before confirming machine suitability.
Die head and downstream equipment
The die controls the initial profile leaving the extruder, but it does not by itself guarantee the final dimensions. Die swell, line speed, cooling, tension, vulcanization and compound shrinkage influence the finished part. For a technically useful proposal, provide the profile drawing, dimensional tolerances, compound data and required line speed.
A complete production process may require a warming mill or other upstream preparation equipment, a temperature-control unit, die tooling, cooling conveyor or bath, haul-off, measuring equipment, cutting system and a suitable vulcanization line. Only equipment listed in the approved quotation is included in MPI’s supply.
Site and utility requirements
- Stable, level foundation with operating and maintenance clearance
- Electrical supply matching the confirmed motor, controls and machine nameplate
- Protective earthing, isolation and over-current protection installed by a qualified electrician
- Clean cooling water or a closed-loop temperature-control system with the required flow, pressure and temperature
- Safe material-preparation and feeding arrangement
- Ventilation and process controls appropriate for the rubber compound and any released fumes
- Space for die changes, screw withdrawal, cleaning and planned maintenance
- Compatible upstream and downstream equipment where the extruder forms part of a line
Installation, commissioning and training
The agreed service scope can include delivery inspection, positioning guidance, electrical and cooling-water checks, gearbox and guarding inspection, no-load rotation, temperature-control checks, trial extrusion and basic operator training. Final acceptance should use an agreed compound, die and operating condition.
Training can cover safe start-up and shutdown, material preparation, die installation, speed adjustment, temperature monitoring, cleaning, routine inspection and first-line troubleshooting. Production recipes remain specific to the customer’s compound and product.
Operating safety and maintenance
The extruder must be operated by trained personnel. The screw, feed opening, coupling, drive, die head and hot or pressurized process areas can cause serious injury. Guards and safety devices must remain installed and functional.
- Isolate and lock out electrical power before maintenance or screw, die and barrel work
- Confirm that head pressure is safely relieved before opening the die or head
- Keep hands and tools clear of the feed opening and rotating components
- Use suitable thermal and chemical personal protective equipment for the compound and process
- Check gearbox oil, bearings, cooling passages, fasteners, guards and electrical connections on schedule
- Do not process an unapproved compound or exceed the confirmed speed, load, pressure or temperature limits
- Follow the final machine manual, compound safety data and site risk assessment
Professional supply in Pakistan
Marjan Polymer Industries supplies rubber and polymer-processing machinery for laboratories, universities, product-development facilities and industrial manufacturers in Pakistan. Support can include application review, custom fabrication, die coordination, installation planning, commissioning, operator training and after-sales service according to the commercial scope.
Customers in Lahore, Karachi, Faisalabad, Sialkot, Islamabad and other industrial locations can submit their compound, profile drawing, target rate, available utilities and factory location for a project-specific single screw extruder proposal.
Information required for a technical quotation
- Rubber type, compound formulation or technical data
- Hot-feed or cold-feed requirement and available upstream equipment
- Required profile drawing and dimensional tolerances
- Target production rate and operating hours
- Required screw diameter or available space, if already defined
- Feed form and expected feed temperature
- Die, head, straining or venting requirement
- Required cooling, haul-off, cutting or vulcanization equipment
- Available electrical and cooling-water utilities
- Factory location and required installation or training scope
Frequently Asked Questions
What is a single screw extruder?
It is an extrusion machine that uses one rotating screw inside a barrel to convey prepared material, build pressure and force it through a die. This product is intended for configured rubber-extrusion applications.
Is the reference machine a rubber extruder?
Yes. The reference 30 mm machine is presented as a compact hot-feed rubber extruder for laboratory, development and controlled small-batch work.
What is the screw diameter of the reference extruder?
The reference screw diameter is 30 mm. Larger or different screw sizes are separate engineered configurations and require application review.
What output can the machine produce?
The reference figure is up to approximately 15 kg/h. Actual output depends on compound viscosity, feed temperature, screw design, die restriction, speed and required extrudate quality.
Can one extruder process every rubber compound?
No. Different compounds can require different screw geometry, materials, temperature control, venting, feed method and die design. MPI confirms compatibility against the stated compound and product.
What is the difference between hot-feed and cold-feed extrusion?
A hot-feed extruder receives pre-warmed and prepared compound. A cold-feed extruder is engineered to accept material closer to ambient temperature. They use different process and machine-design assumptions.
Can MPI provide a custom die or extrusion head?
Yes. Die and head requirements can be reviewed from the profile drawing, compound information and required tolerances. Tooling is included only when stated in the quotation.
Is downstream equipment included?
Cooling, haul-off, cutting and vulcanization equipment can be quoted when required, but they are not automatically included with the extruder.
Is the single screw extruder available in Pakistan?
Yes. Marjan Polymer Industries can supply configured single screw extruder machines in Pakistan, subject to the approved technical and commercial proposal.
Are installation and operator training available?
Yes. Installation, commissioning and operator training can be included according to the agreed site and service scope.
Request a single screw extruder proposal
Contact Marjan Polymer Industries with your rubber-compound information, profile drawing, target output and factory location. MPI will review the application and prepare a suitable machine configuration and quotation.