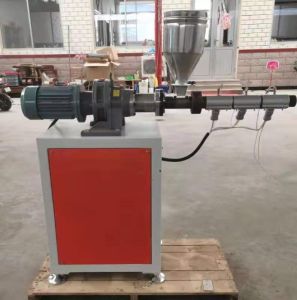
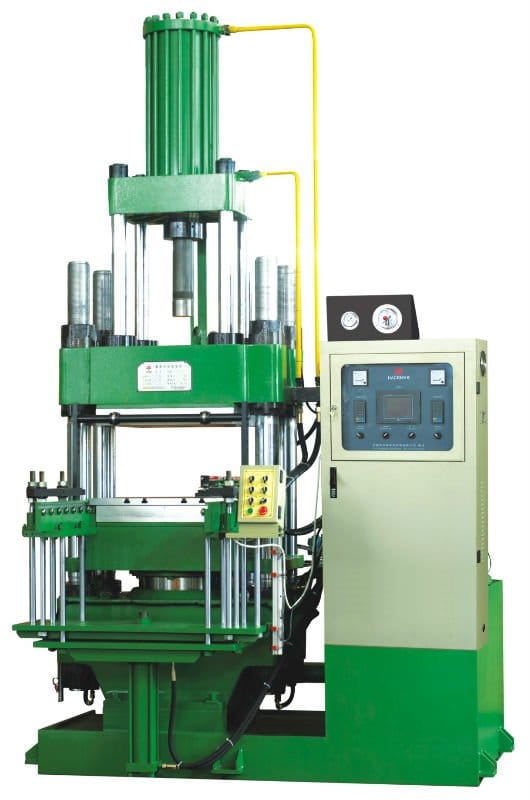
A Rubber Injection Molding Machine meters, plasticises and injects an uncured elastomer compound into a temperature-controlled mould, holds the mould under clamping force during vulcanisation and supports repeatable demoulding. Marjan Polymer Industries (MPI) supplies project-engineered vertical or horizontal rubber injection systems, tooling interfaces, controls, installation and support for manufacturers in Pakistan.
Rubber injection differs materially from conventional thermoplastic injection moulding. Compound rheology, scorch safety, injection-unit temperature, mould heating, cure time, cold-runner design, venting and flash control must be engineered for the selected elastomer and part.
Process Purpose
The process aims to deliver a controlled compound mass to every cavity, maintain a uniform mould temperature and clamp force, complete the defined cure and remove the part safely. Repeatability depends on the compound batch, feed geometry, plasticisation, shot metering, injection pressure/speed profile, mould design, venting and cure control.
Machine Configurations
| Configuration | Typical use | Engineering options |
|---|---|---|
| Vertical top injection | Flexible rubber and silicone moulding with accessible mould area | Fixed or moving lower bolster, top nozzle, shuttle or slide table |
| Vertical side injection | Parting-line injection, stack moulds and short flow paths | Retractable injection unit and cold-runner interface |
| Horizontal machine | High-volume automated production and inline handling | Robot take-out, conveyor, trimming and inspection integration |
| Injection-transfer system | Applications combining injection metering with transfer-style tooling | Top/bottom arrangement, vacuum and multi-station mould handling |
| LSR/HTV package | Silicone-specific processing | Metering/stuffer, cooled feed zone and material-specific injection unit |
Configurable Technical Range
| Parameter | Common project class | Selection basis |
|---|---|---|
| Clamping force | Approximately 1,000–10,000 kN for common industrial projects; smaller and larger special systems by review | Projected cavity area, cavity pressure, number of cavities, runner and safety factor |
| Injection volume | Approximately 100–5,000 cm³ for common systems; larger special volumes by review | Part/runner mass, compound density, cushion and refill cycle |
| Injection pressure | Application-selected high-pressure class, commonly up to approximately 1,500–2,500 bar | Compound viscosity, flow length, gate, cavity geometry and injection unit |
| Heated platen/mould range | Typically approximately 80–220 °C with multi-zone control | Elastomer cure system, mould mass, uniformity and process recipe |
| Mould daylight and stroke | Project-defined | Mould stack, loading/demoulding access, ejector and automation |
| Control | PLC/HMI with recipe, trends, alarms and interlocks | Process complexity, traceability and plant interface |
Injection Unit and Compound Handling
- FIFO or application-selected injection architecture for controlled residence time and shot repeatability.
- Strip, preform, silicone or other feed arrangement matched to compound presentation.
- Temperature-controlled barrel/nozzle strategy to reduce premature cure while maintaining stable flow.
- Liftable or retractable nozzle and purge/cleaning provisions where required by mould access.
- Closed-loop control of injection speed, pressure, position and hold profile where included.
Clamping, Heating and Mould Interface
| System | Design considerations |
|---|---|
| Clamping unit | Deflection resistance, pressure distribution, opening force, stroke and safe mould access |
| Platen heating | Zone layout, temperature uniformity, insulation, warm-up and sensor placement |
| Vacuum | Vacuum chamber or mould connection for trapped-air and filling control |
| Cold runner | Compound saving, temperature separation, balance and cleanability |
| Ejection | Hydraulic/mechanical ejector, core pulls, brush, stripper or robot interface |
| Mould change | Rails, lifters, quick clamps, preheating and connection management |
Control and Process Data
- Recipe control for injection, clamp, cure, vacuum, temperature and demoulding sequence.
- Position, pressure, speed, temperature and cure-time monitoring with alarm limits.
- User levels, change log and batch/shot data options for controlled production.
- Remote service, plant data interface and energy monitoring where approved.
- Custom automatic sequence for mould, core, brush, ejector, robot and conveyor functions.
Rubber and Silicone Applications
- Natural rubber, SBR, NBR, EPDM, CR and selected specialty elastomers.
- Automotive seals, gaskets, boots, bushes, diaphragms and vibration-control parts.
- Rubber-to-metal bonded components, electrical parts, footwear and industrial articles.
- Medical/pharmaceutical elastomer components only with the required cleanroom, material and validation package.
- HTV and liquid silicone rubber with material-specific feeding, metering and temperature control.
Safety and Compliance Philosophy
The machine scope can include interlocked guards/doors, light curtains or area scanners where appropriate, emergency stops, safe hydraulic/servo monitoring, platen and hot-surface protection, controlled mould access and energy isolation. The final safeguards are based on the machine layout, automation, mould and applicable risk assessment. Customer tooling must also meet the approved safety interface.
Factory Acceptance and Documentation
| Deliverable | Typical scope |
|---|---|
| Design package | General arrangement, foundation/load data, platen/mould interface, utilities and control architecture |
| Machine FAT | Clamp, injection, heating, controls, alarms, guards and dry-cycle checks against protocol |
| Mould trial | Customer compound and production mould trial only when agreed material, tooling, method and acceptance criteria are available |
| Documents | Electrical/hydraulic drawings, operation/maintenance manual, lubrication and spare-parts list |
| Training | Operation, recipe setup, safety, mould change and preventive-maintenance instruction as quoted |
Information Required for a Proposal
- Part drawing, weight, projected area, cavity count and quality requirements.
- Rubber or silicone grade, Mooney/rheology data, feed form, cure curve and safety data.
- Mould drawing, runner system, dimensions, weight, heating, core and ejector functions.
- Required output, cycle target, working shifts, automation and traceability level.
- Utilities, floor space, lifting, mould-change method and Pakistan installation location.
Installation and After-Sales Support
MPI can provide site-interface review, installation supervision, commissioning, training, preventive-maintenance planning and spare-parts coordination in Pakistan. Process acceptance requires the agreed compound, mould, utilities and measurement method to be available.
Frequently Asked Questions
What is a Rubber Injection Molding Machine?
It is a machine that meters and injects uncured rubber or silicone into a heated mould, applies clamping force during filling and vulcanisation, and controls the cycle until the part can be demoulded.
How is rubber injection moulding different from plastic injection moulding?
Thermoplastics are melted in a heated barrel and cooled in the mould. Rubber compounds must be protected from premature cure in the injection unit and then heated in the mould to vulcanise, so the temperature and tooling strategy are different.
Should the machine be vertical or horizontal?
The part, mould, injection point, demoulding method, insert loading, automation and available floor space determine the orientation. Vertical top or side injection is common for elastomers, while horizontal machines suit selected automated production.
What clamping force is required?
Clamp force is calculated from projected cavity and runner area, expected cavity pressure, cavity count and safety factor. Part weight alone is not a valid sizing method.
Which rubber compounds can be processed?
Natural and synthetic rubbers including NR, SBR, NBR, EPDM and CR can be evaluated. FKM, HTV silicone, LSR and specialty compounds require material-specific injection, temperature and handling review.
Can MPI supply vacuum and cold-runner options?
Yes. Vacuum chambers or mould connections, cold-runner blocks, ejectors, core pulls, shuttles and mould-handling options can be included when justified by the tooling and process.
Can an existing mould be used?
Possibly. MPI must review mould dimensions, weight, projected area, injection position, heating, ejector/core functions, clamping interface and process requirement before confirming compatibility.
Can process data be recorded?
PLC/HMI systems can provide recipe control, alarms, trends, user levels and shot-data options. The exact signals, storage and plant interface are defined in the control specification.
Does MPI provide installation in Pakistan?
MPI can provide installation supervision, commissioning, training and after-sales support in Pakistan according to the approved project scope.
What is required for a quotation?
Provide the part and mould drawings, compound data and cure curve, cavity count, required output, automation, utilities, floor space and installation location.
Request a Rubber Injection Molding Machine Proposal
Send MPI your part, mould and compound data, target output, automation requirement and site conditions. Marjan Polymer Industries will prepare a project-specific Rubber Injection Molding Machine proposal for your manufacturing facility in Pakistan.